

Laser Cut Finishes
Get the Right Finish — The First Time
Fast, precise laser cutting is only part of the equation.
Choosing the correct finish ensures your parts meet function, fit, and appearance requirements.

STEP 1: What Matters Most for Your Part?
Choose your priority:
🔧 Function (internal / non-visible)
✋ Safe handling (no sharp edges)
👁 Cosmetic appearance
🎨 Finished product (coated / final use)
STEP 2: Recommended Finish Based on Your Goal
Finish Options (Quick Selection Guide)
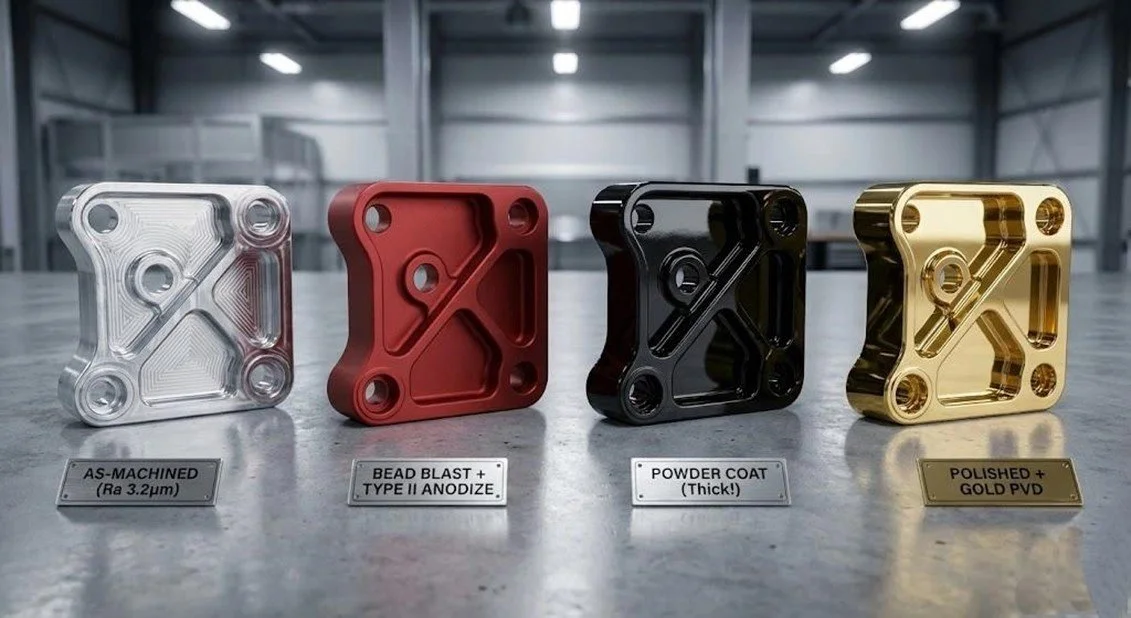
🔧 As-Cut
Fastest turnaround
Lowest cost
Visible edge texture
🧹 Deburred
Smooth edges
Safe to handle
Most common option
✨ Tumbled
Uniform matte finish
Softened edges
Cosmetic improvement
🎯 Brushed
Directional grain
Premium visual appearance
🎨 Powder Coated
Final product finish
Durable + corrosion resistant
As-Cut vs Finished Comparison


STEP 3: Design Validation (Prevents Issues Before Quoting)
📏 Tolerance Guide (Based on Thickness)
Minimum hole size = 60% of material thickness
Example:
🕳️ Hole Size Rule (CRITICAL)
⚠ If your design is below this:
Expect poor edge quality
May require machining
Will be reviewed at quoting

Common Issues (Avoid These)
Holes too small
Expecting cosmetic finish without specifying it
Tight tolerances on laser-only features
Ignoring edge condition
What You Get with Max Machining
⚡ Fast turnaround (same-day capable)
📐 Real DFM feedback before production
🔩 Scalable production capability
US Manufactured in Bucks County Pennsylvania


Ready to Start Your Project?
Take the next step toward precision manufacturing with Max Machining. Whether you have a 2D drawing, a 3D model, or just a concept, our team is ready to provide a fast, accurate quote and guide your project from design to production. Partner with a compliant, trusted, and experienced manufacturing team that delivers quality, speed, and reliability every time.